
Short arc and drawn arc welding equipments
9 products available
Short-cycle and drawn arc stud welding for threaded studs, bushes and industrial metal fabrication
Short-cycle and drawn arc stud welding machines are used to attach threaded studs, internally threaded bushes, shear connectors and other metallic fasteners to sheet metal, fabricated structures and industrial components. The welding method must be selected according to the stud diameter, base material, component thickness and mechanical requirements of the finished joint.
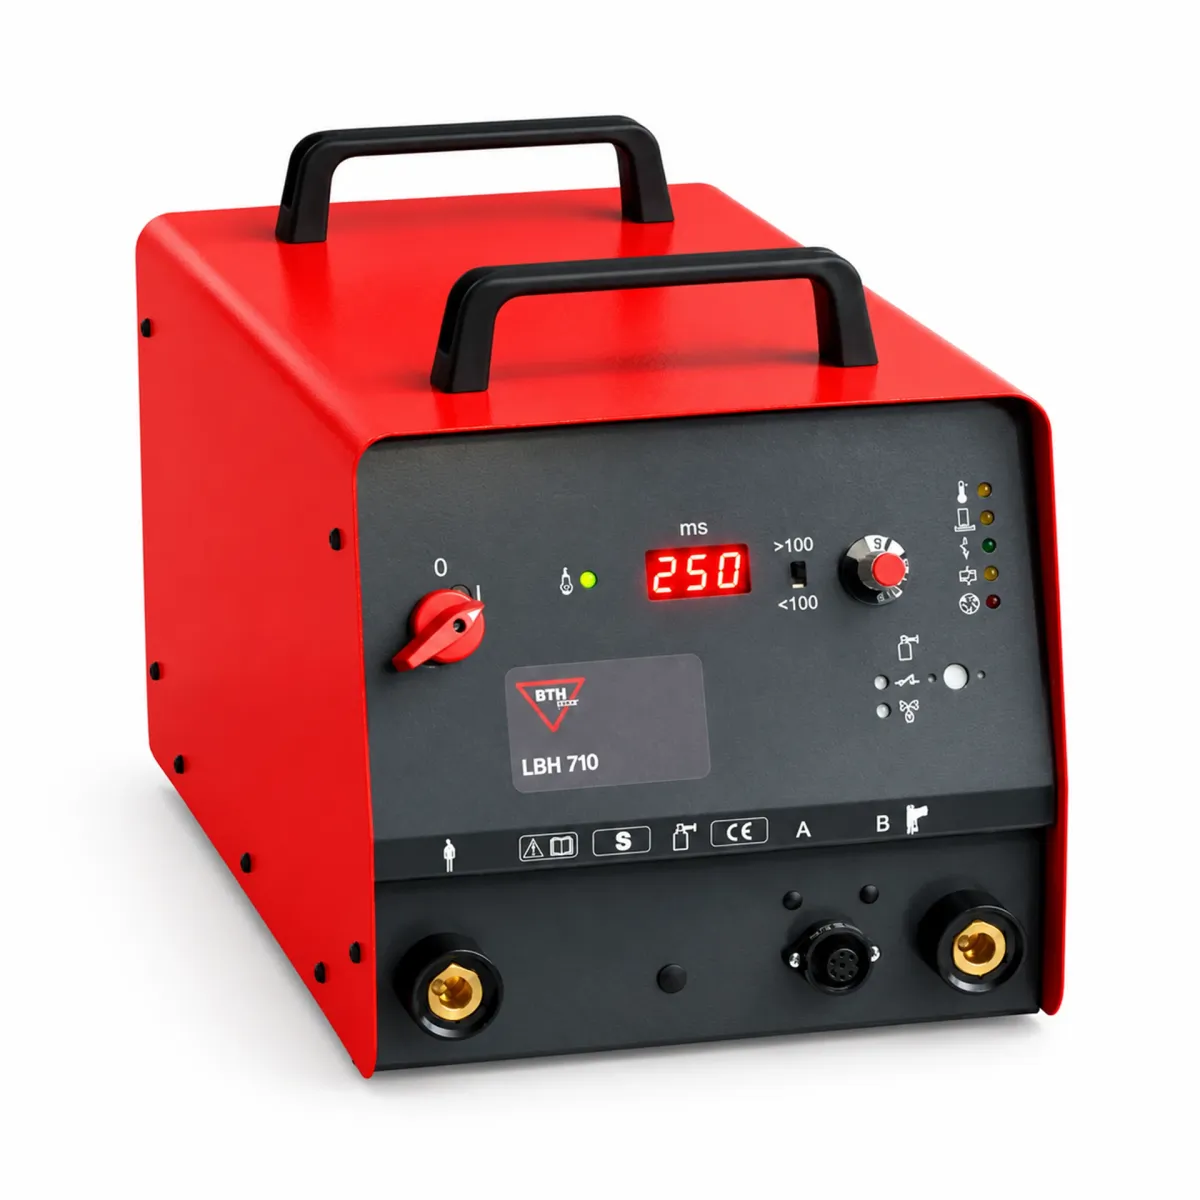
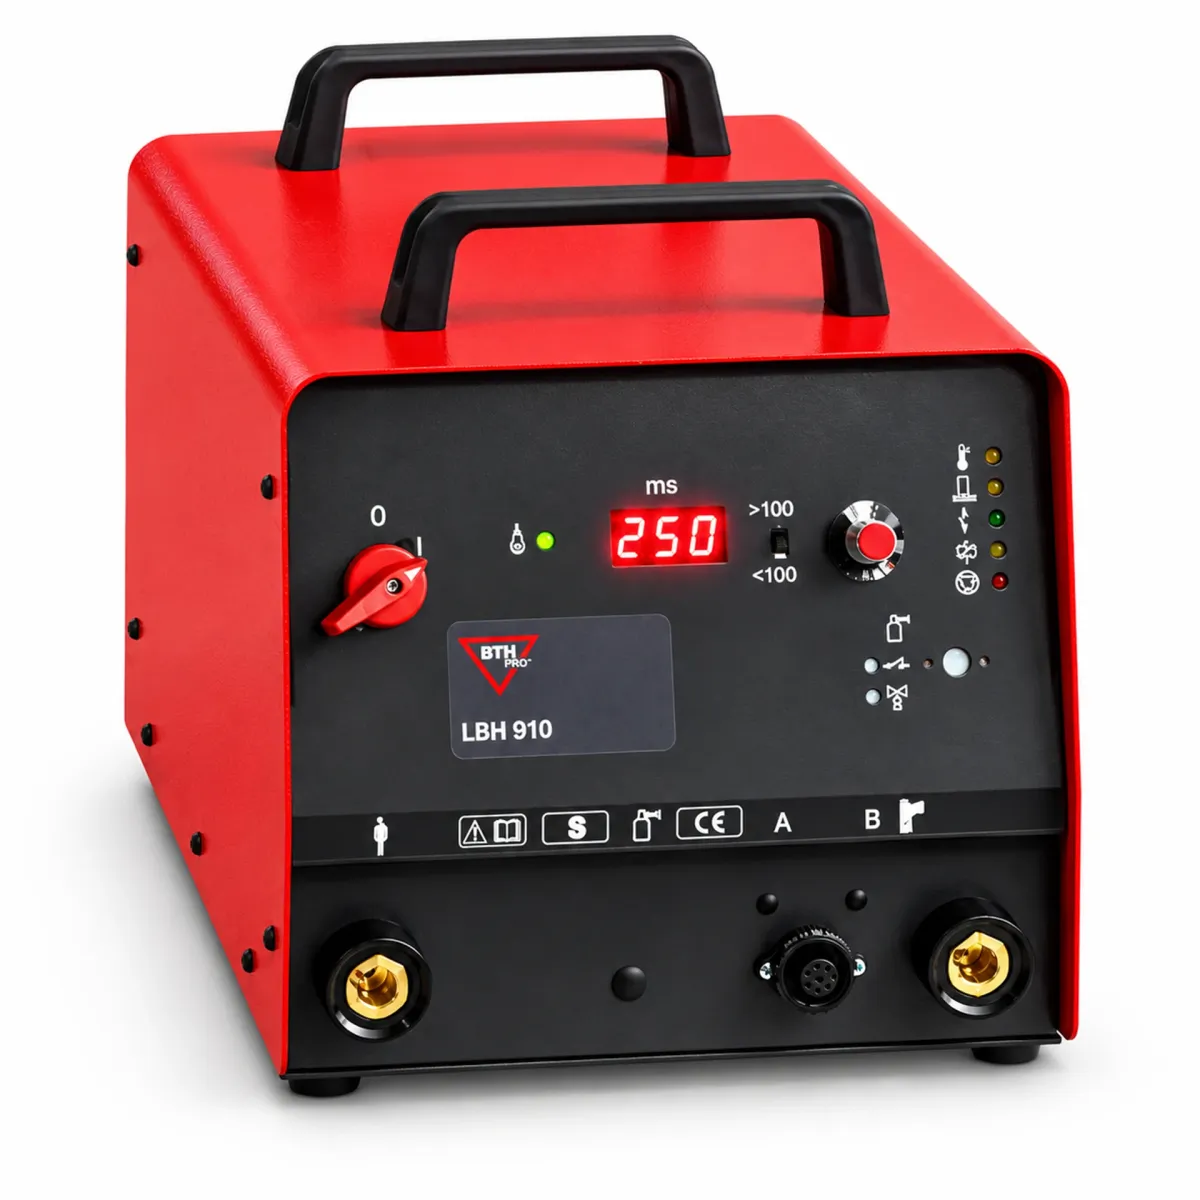
A.T.S. supplies arc stud welding equipment from the LBH, PRO-D and PRO-I ranges. The machines cover different welding capacities and operating requirements, from manual workshop applications to systems that can be configured for automated production. Conventional power sources and inverter-based machines are available, with control and monitoring functions depending on the model.
Drawn arc stud welding with ceramic ferrules
In drawn arc stud welding, an electric arc is established between the stud and the workpiece. The arc melts the end of the stud and part of the base material before the stud is driven into the molten weld pool, allowing the two materials to join.
A ceramic ferrule is often used to surround the weld area. It helps contain the molten metal and provides protection during the welding cycle. This arrangement is widely used for studs and shear connectors in steel fabrication, structural components and applications requiring permanent welded fixings.
The ferrule must be matched to the stud geometry, and sufficient clearance is required around the welding position. Welding current, arc time and stud movement must also be adjusted to the material and fastener dimensions.
Gas-shielded drawn arc welding
For suitable applications, the welding area can be protected using a shielding gas instead of a ceramic ferrule. The gas reduces the exposure of molten metal to the surrounding atmosphere during the weld.
This method can be useful where the geometry of the component or the required welding arrangement makes gas shielding appropriate. However, the welding power source, gun and gas delivery accessories must all support the selected process.
A.T.S. describes gas-shielded configurations for studs up to 12 mm in diameter, depending on the equipment. This figure is application-specific and should not be interpreted as the maximum welding capacity of the complete arc welding range.
Short-cycle stud welding for thinner materials
Short-cycle arc stud welding uses a shorter arc duration than conventional drawn arc welding. Reducing the welding time can help limit heat input to the component, making the process suitable for certain thinner sheet metal applications.
The A.T.S. range includes configurations for PD-type threaded studs up to M8 and ID-type internally threaded bushes. These are examples of compatible applications rather than a universal size limit for every short-cycle machine.
Short-cycle welding must be assessed against the required joint strength, sheet thickness, material and stud geometry. A shorter cycle does not automatically guarantee better results than capacitor discharge welding or conventional drawn arc welding. The appropriate procedure depends on the actual joining requirements.
LBH, PRO-D and PRO-I welding machines
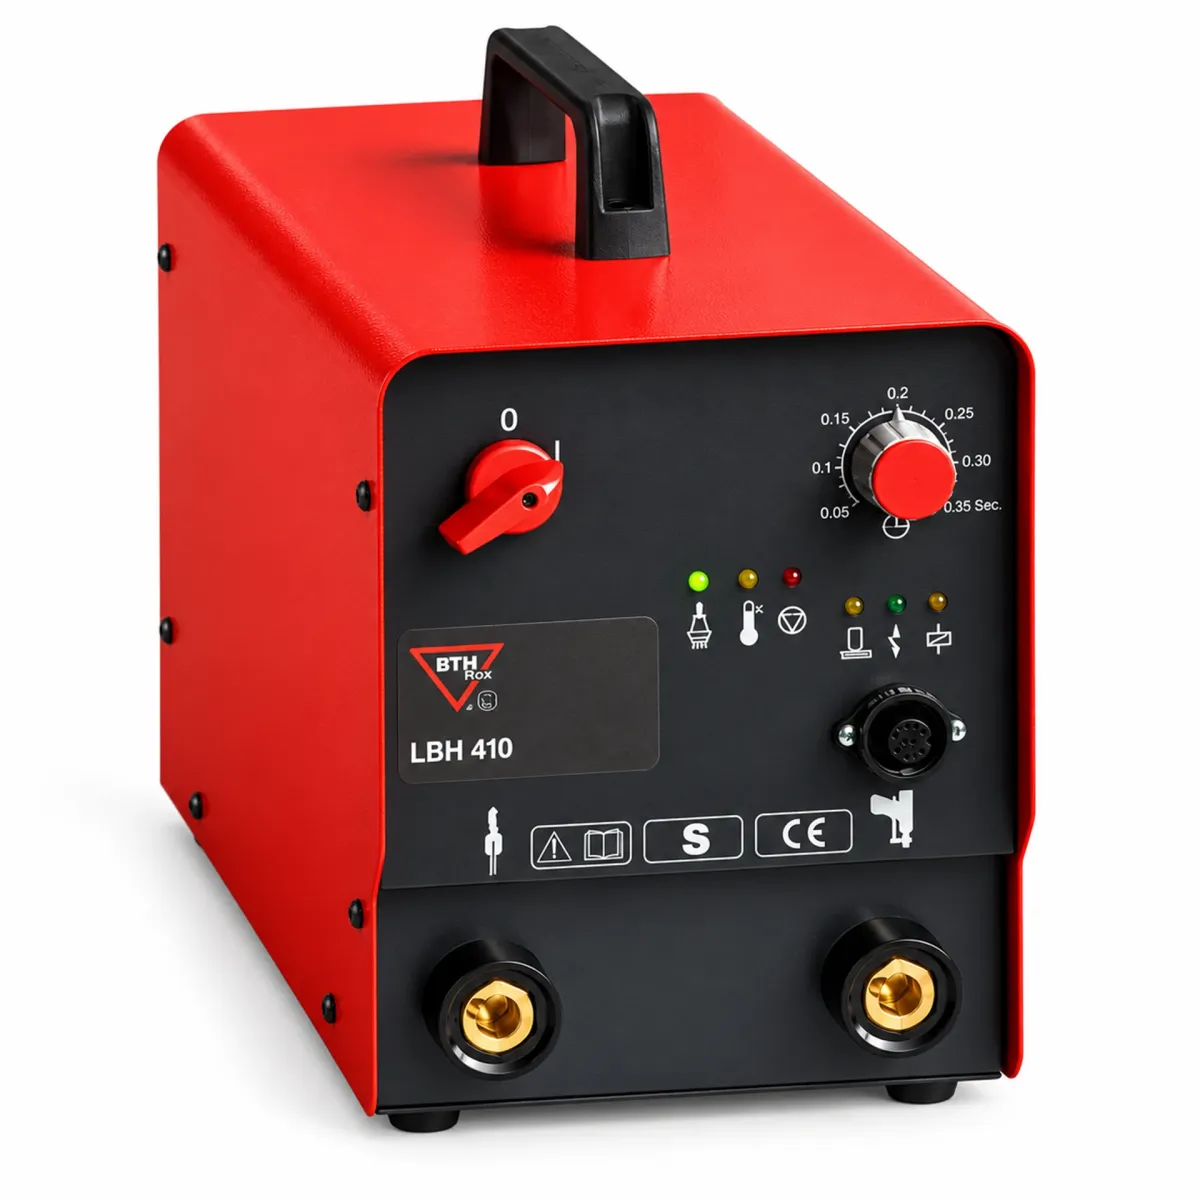
The LBH series includes arc stud welding machines with different welding capacities. For example, the LBH 410 is specified for diameters from 2 to 8 mm using ceramic ferrules. It is not intended for short-cycle or gas-shielded operation.
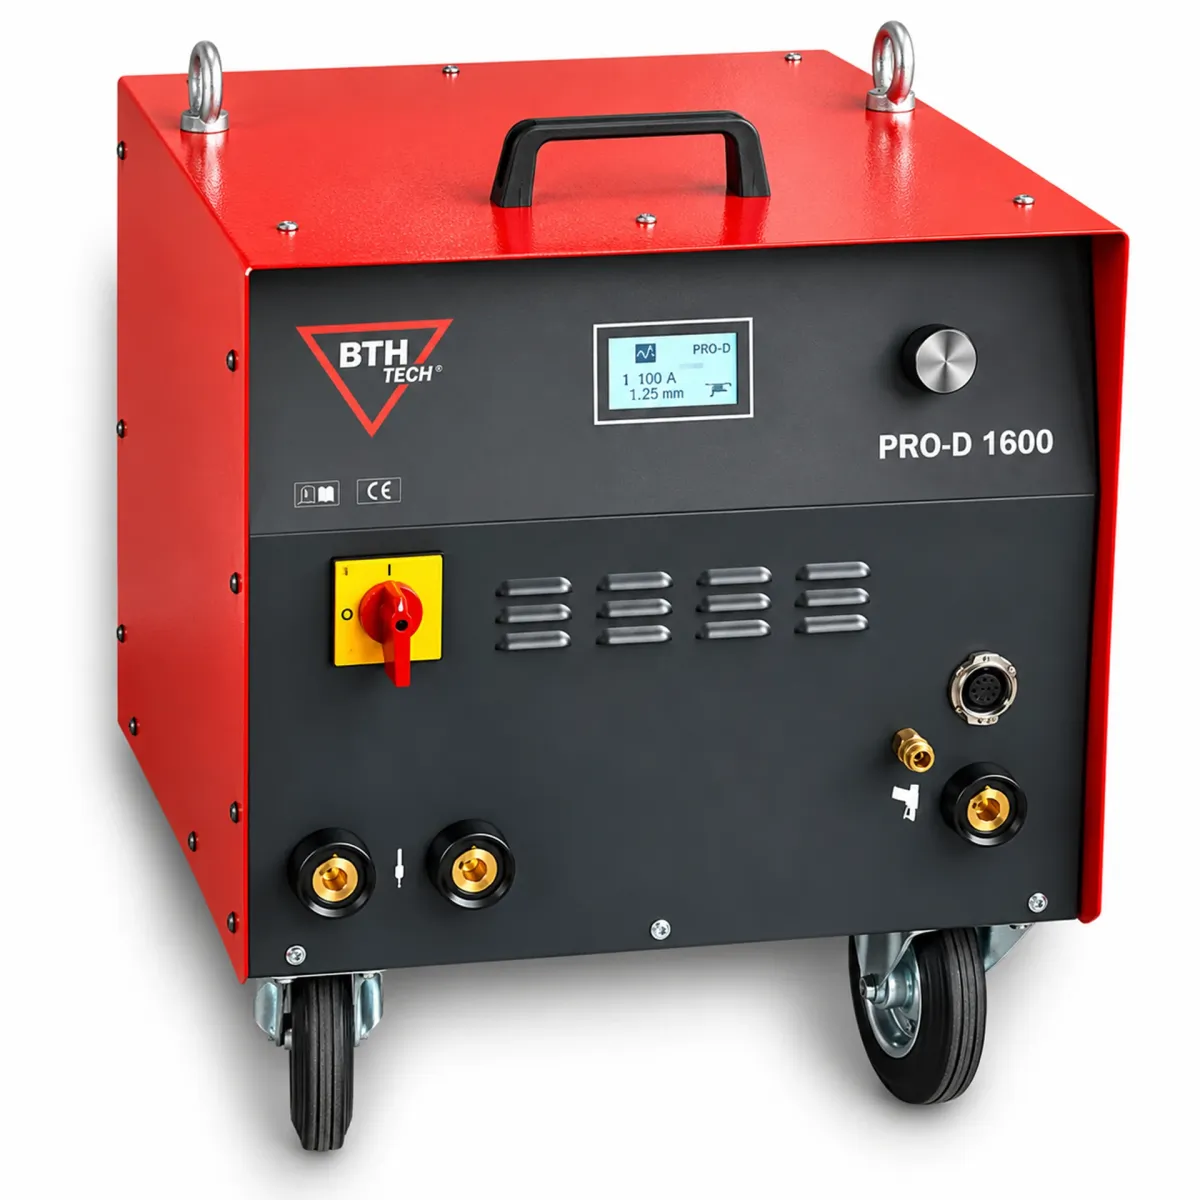
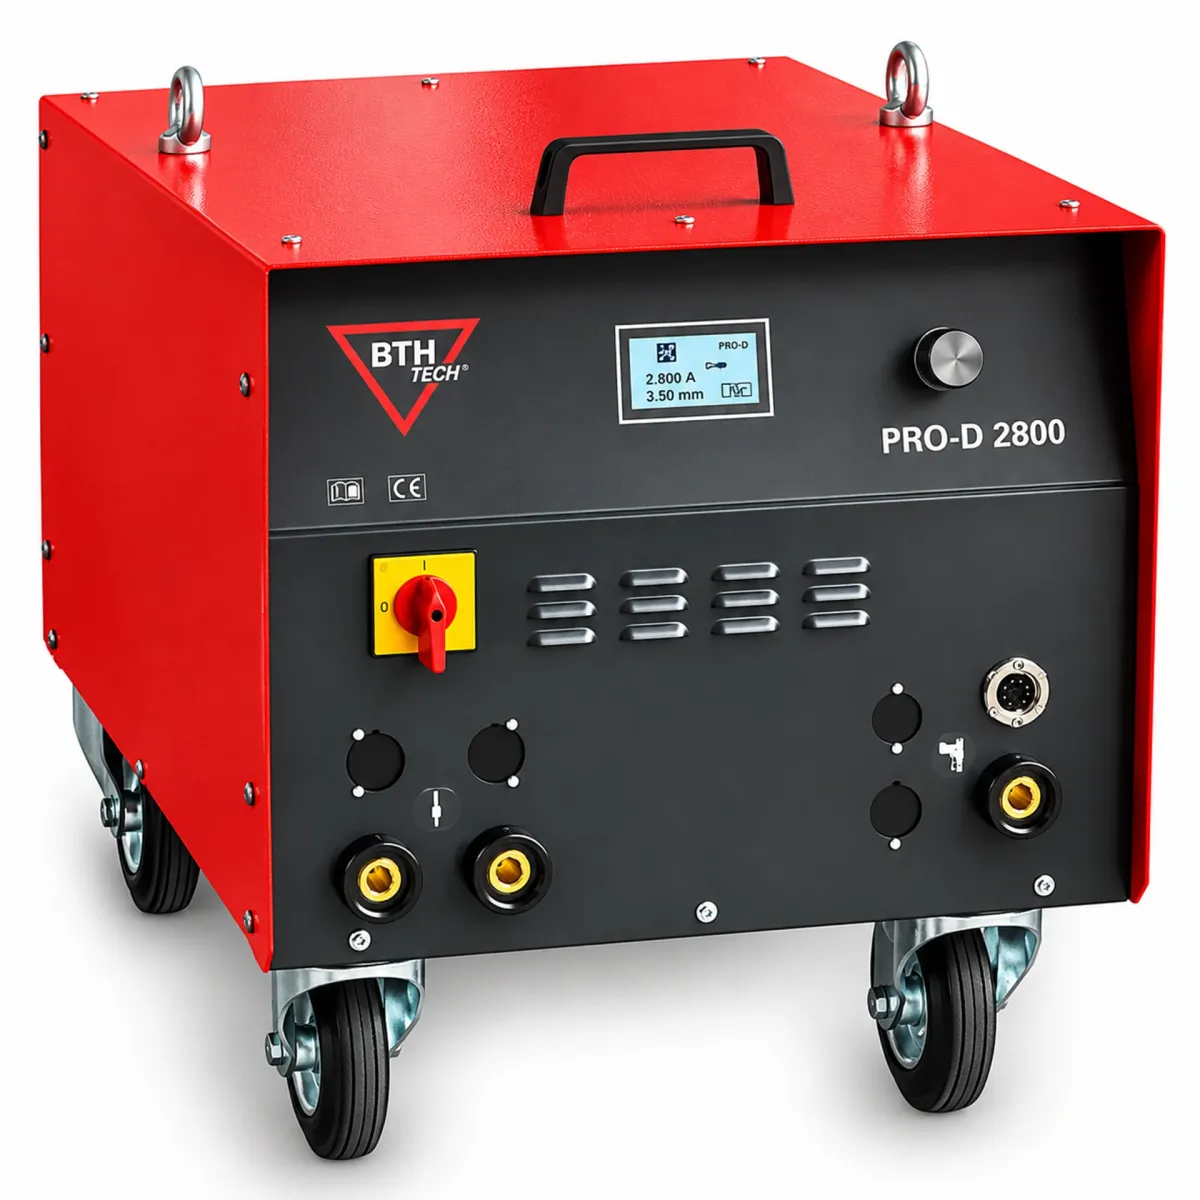
The PRO-D series includes microprocessor-controlled equipment with adjustable welding current and time. Selected models offer stored programmes, process monitoring and optional integration accessories. The PRO-D 1600, with a specified welding range of 2–16 mm, supports short-cycle and drawn arc applications and can be equipped for gas-shielded welding.
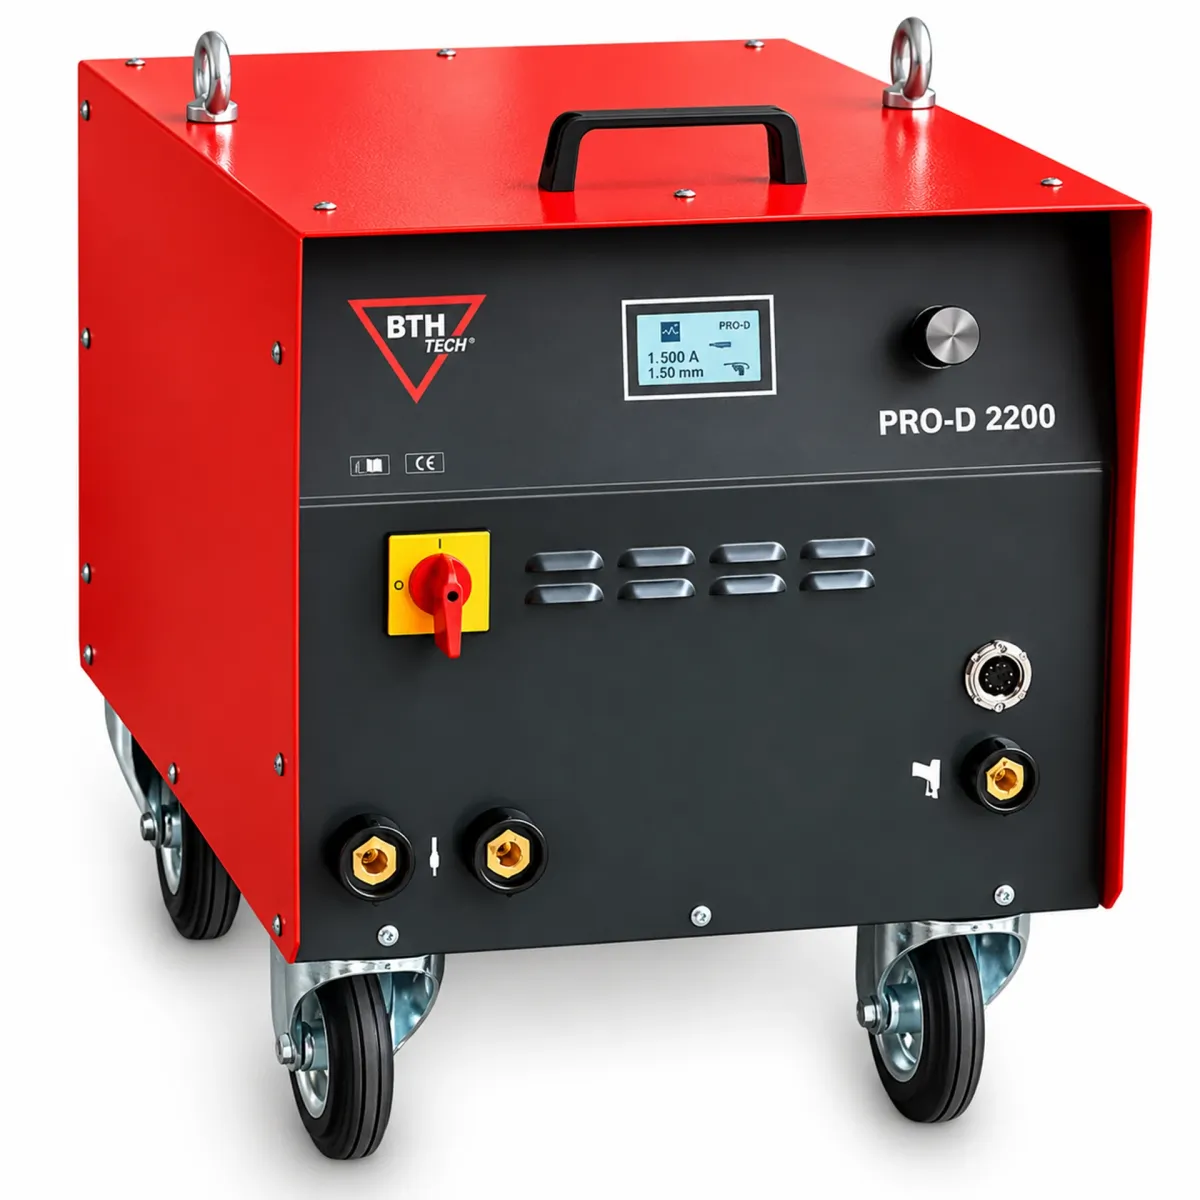
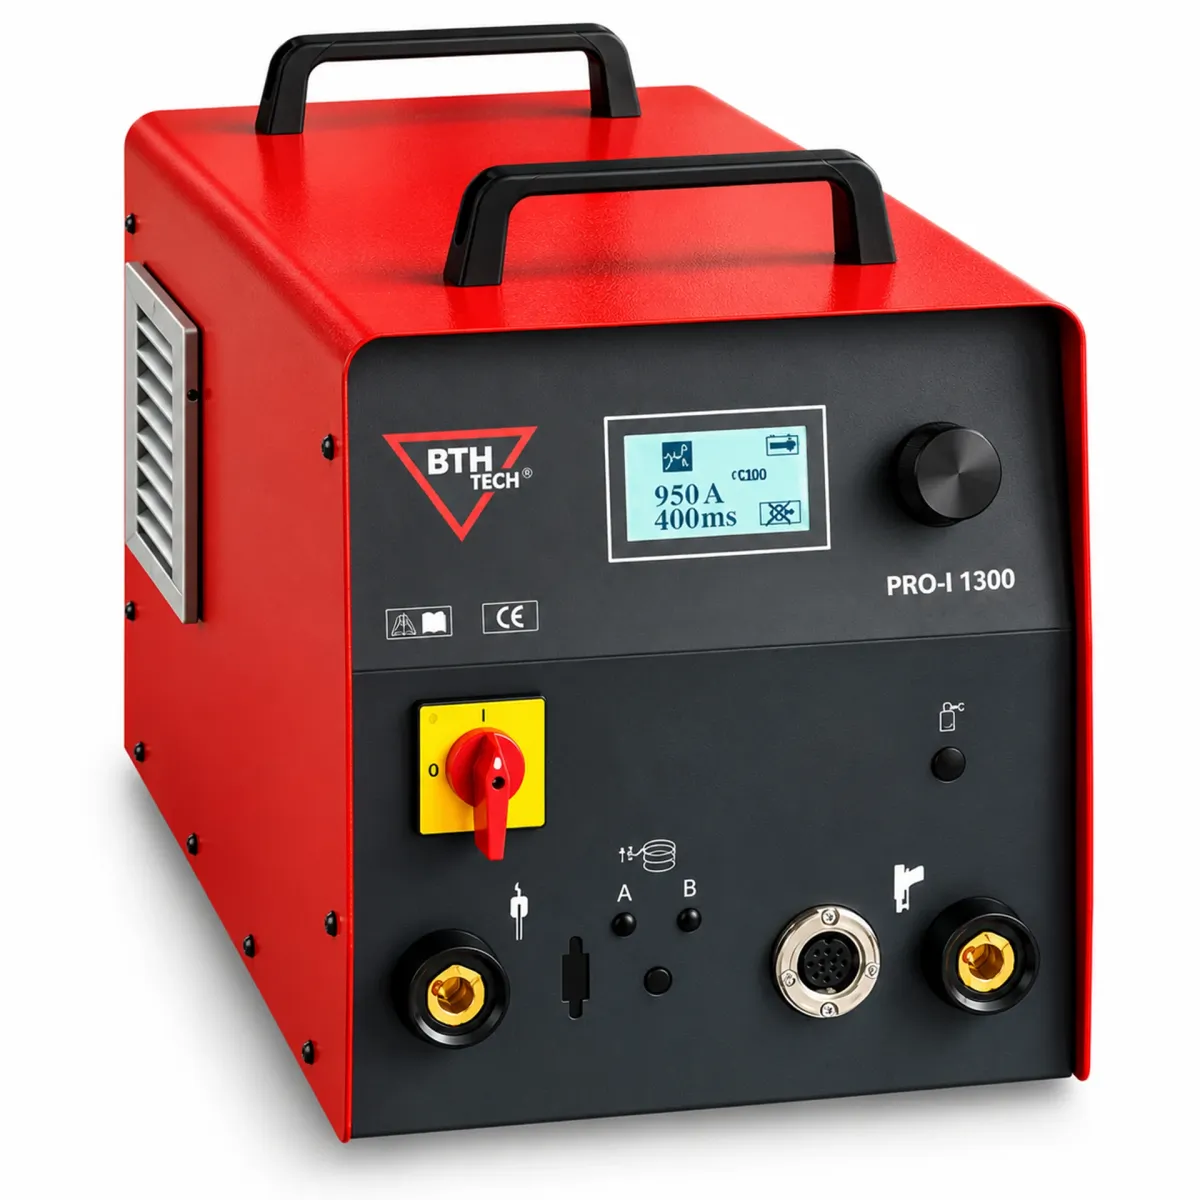
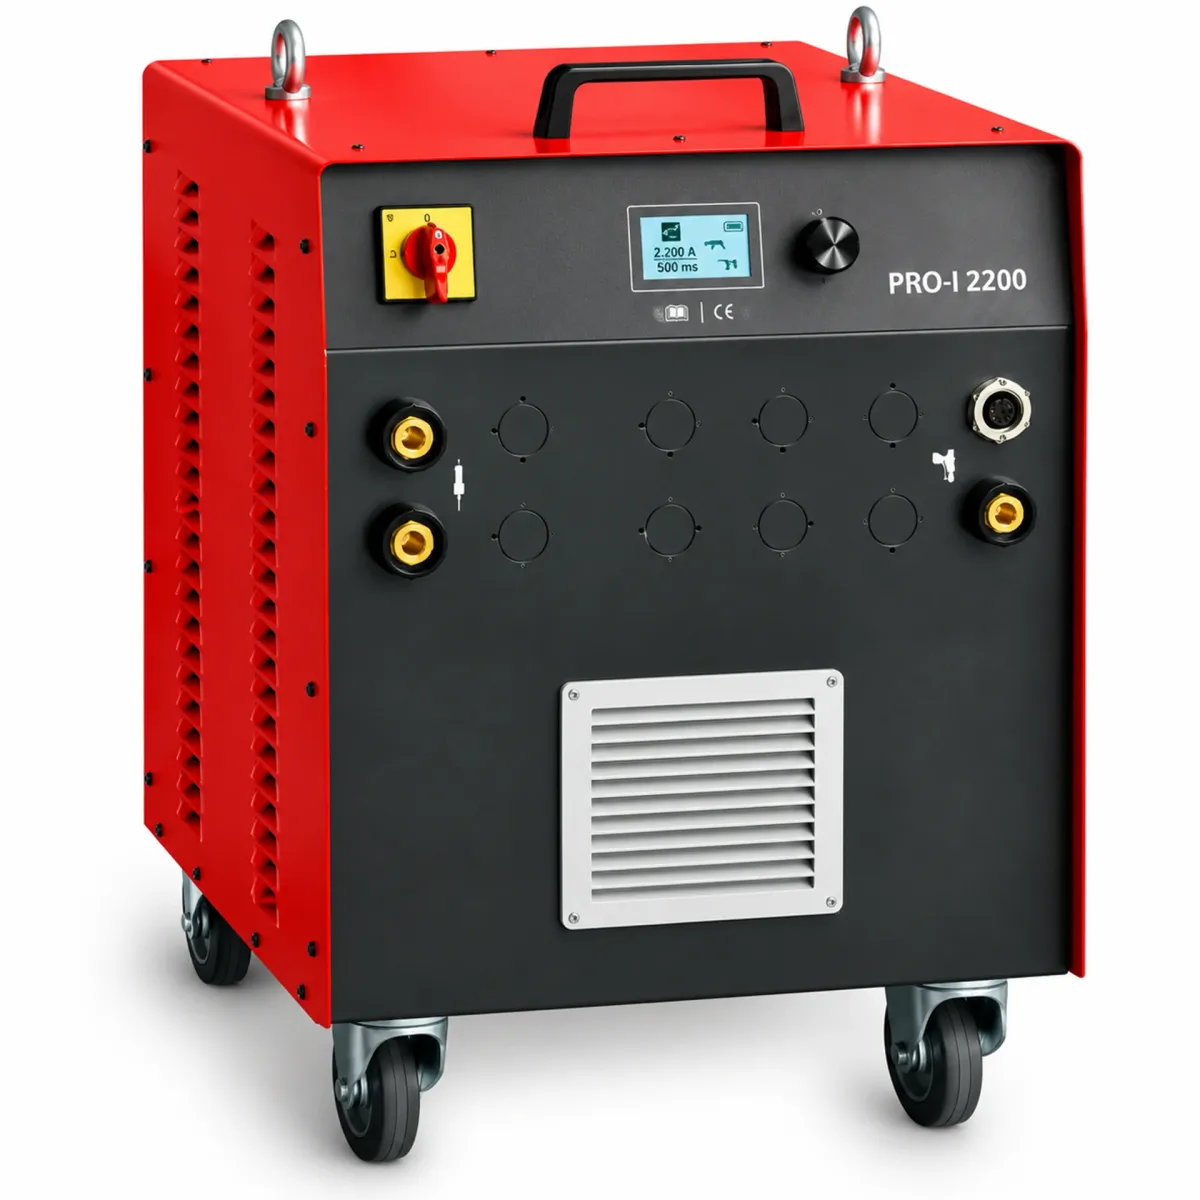
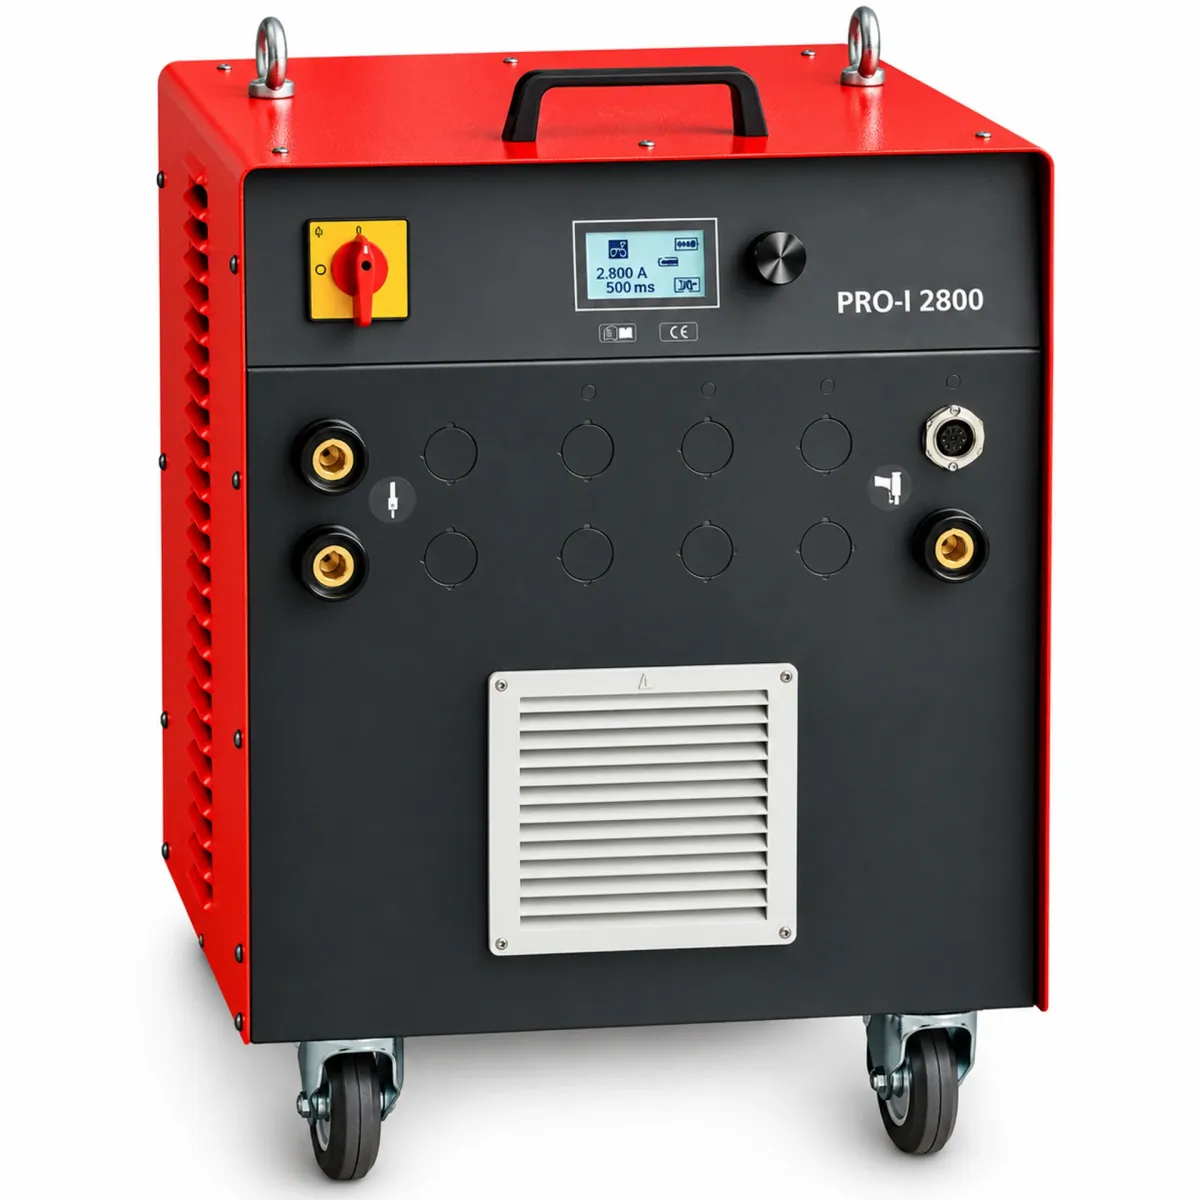
The PRO-I series uses inverter technology to control welding current. Depending on the model, these machines can offer extended welding capacities, electronic parameter control and interfaces for specialised production equipment. The PRO-I 2200, for example, supports optional stud feeding, automatic welding heads and multiple welding guns through compatible accessories.
These differences should be considered when selecting a machine; control functions and automation options are not identical across the complete range.
Welding guns, studs and industrial applications
A.T.S. supplies manual short-cycle and drawn arc stud welding guns for different fastener dimensions and welding methods. The gun must be compatible with the power source, stud diameter and use of ceramic ferrules or shielding gas where required.
The available weld studs and welding fasteners include threaded studs, internally threaded bushes and shear connectors. Their geometry and material must be suitable for the chosen welding process and the loads expected in service.
Arc stud welding is used in structural steelwork, general metal fabrication, machinery manufacturing and shipbuilding. Short-cycle arrangements are also suitable for selected sheet metal applications where limiting the welding heat input is important.
A.T.S. provides technical guidance for selecting short-cycle and drawn arc stud welding machines, considering stud dimensions, base material, welding method, component thickness and production requirements. Matching the power source, gun and fastener helps establish suitable welding conditions and supports repeatable joint quality.
The drawn arc stud welding is a process of union between a metal threaded stud on a metal surface through the use of special equipment that by the welding gun, activates an electric arc which melts the tip of the stud and the surface below creating a weld bath that is contained within a ceramic ferrule.
In the long arc cycle welding the welding stud or pin are welded by an electric discharge that melts the material and the melting bath is contained either in a ceramic ferrule or remains free cooled by an inert gas that is automatically activated inside a protective positioner placed on the gun.
In the short arc cycle welding the electric arc is generated in a time of a few ms, this results in much lower melting material than long arc cycle welding and is mainly used to weld threaded studs up to M8 on thin sheet metal.
At A.T.S. Lamberti we offer a wide range of welding machines suitable for drawn arc welding works such as welding shear connectors used in mechanical carpentry, the long cycle welding studs in shipbuilding. Normally the drawn arc welding machines that supplies A.T.S are used for processing medium-heavy carpentry instead, short cycle stud welding is mainly used in the automotive industry such as welding thin sheets or in difficult positions.
The key elements include a careful cleaning of surfaces, the choosing of the correct equipment that normally A.T.S. advises to the customer, a proper adjustment of welding parameters, and the use of certified drawn arc welding studs.
The right solution for your application, with the support of our experts
Our experts will help you find the right product for your needs, with no obligation. Tell us what you need: together we will find the most suitable solution.
Contact us, no obligation