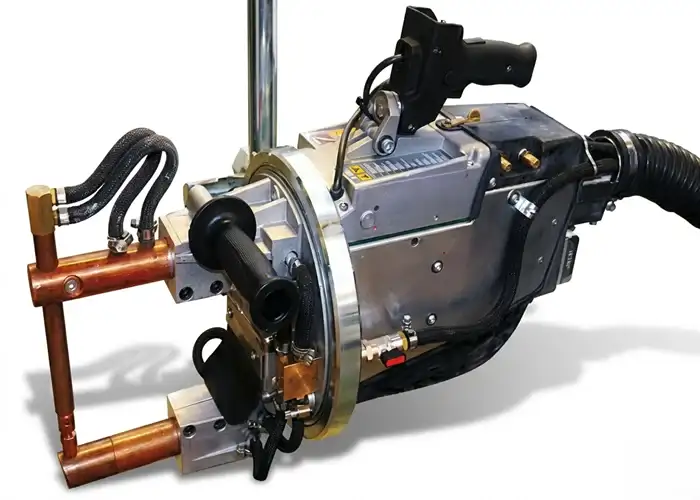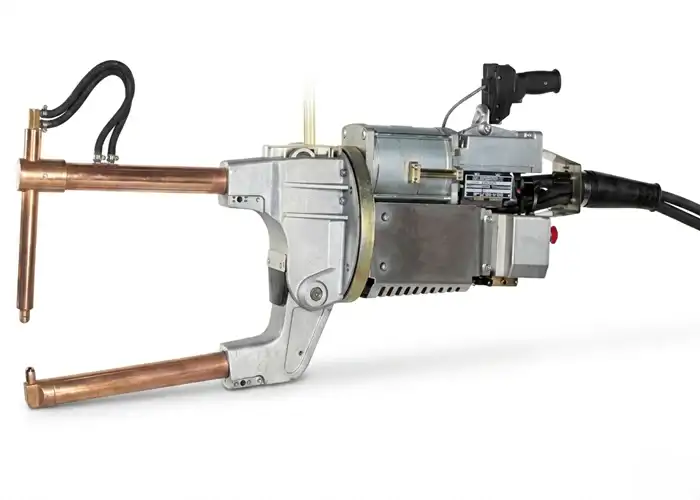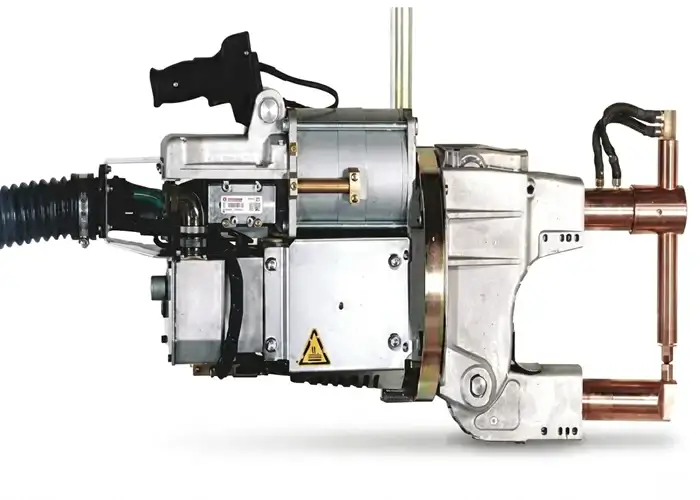

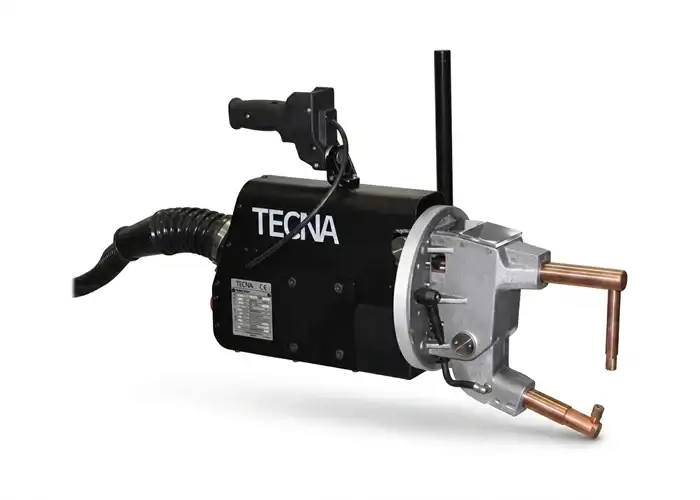
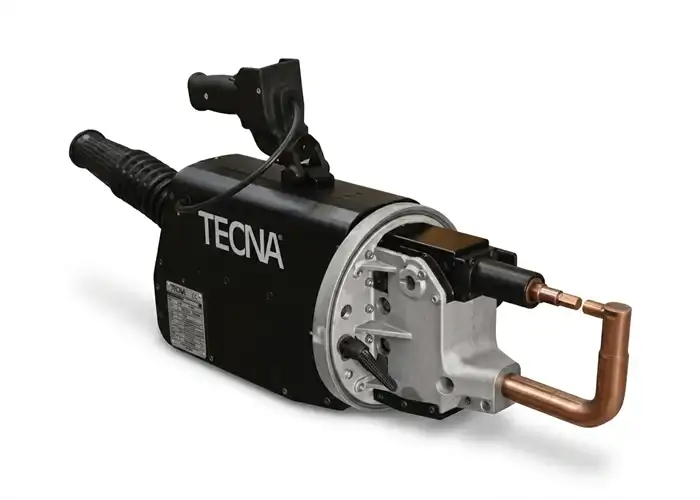
MFDC Suspended Spot Welding Guns 3230 - 3233 – 50 kVA
Medium frequency inverter spot welding guns for industrial resistance welding applications, delivering consistent weld quality, process stability and reliable production performance.
When consistency, weld quality and production efficiency are critical, MF inverter suspended spot welding guns offer a significant advantage over conventional AC resistance welding equipment. Models 3230 and 3233, rated at 50 kVA, are designed for manufacturers looking to achieve stable welding performance, minimise process variation and maintain repeatable results throughout high-volume production.
By using Medium Frequency (MF) inverter technology, these suspended spot welding guns deliver a more controlled welding current, helping to produce uniform weld nuggets while reducing energy consumption and unnecessary heat input. This makes them particularly suitable for applications where weld quality, repeatability and production uptime are essential.
From automotive body assemblies and sheet metal fabrication to domestic appliances, electrical enclosures and general metal manufacturing, resistance spot welding remains one of the fastest and most reliable joining processes. Choosing the correct welding gun, however, involves much more than selecting the required power rating. Material type, sheet thickness, electrode force, arm configuration and production layout all influence the final welding performance.
ATS supports manufacturers throughout the selection process, helping identify the most appropriate solution for each application. Rather than simply supplying equipment, ATS provides technical advice, assistance with machine configuration, support when selecting welding arms and electrodes, and after-sales technical assistance to ensure the equipment matches real production requirements.
Both the 3230 and 3233 models provide a nominal output of 50 kVA at 50% duty cycle (80 kVA at 20%) and are engineered to maintain stable welding current throughout every cycle. The result is improved weld consistency, reduced reject rates and lower operating costs compared with traditional AC spot welding systems.
The 3230 version is intended for applications requiring higher electrode force. It features a 155 mm throat gap, delivers up to 380 daN electrode force at 6 bar, provides a 19 kA short-circuit current and accepts 28 mm arm fittings. The 3233 model incorporates a 0–40 mm double stroke, develops 300 daN electrode force at 6 bar, maintains the same 19 kA short-circuit current and uses 34 mm arm fittings, making it a practical choice where additional operating flexibility is required.
A wide range of welding arm configurations allows the equipment to be adapted for different components and production layouts. Selecting the correct arm length is important not only for reaching the weld location, but also for maintaining the appropriate electrode force and ensuring consistent weld quality throughout the production cycle.
MF inverter technology is particularly beneficial when welding mild steel, galvanised steel, stainless steel and other materials commonly used in modern manufacturing. Accurate control of welding current helps minimise distortion, improve weld appearance and maintain consistent results even during continuous production.
The welding guns are operated via a dedicated medium frequency control cabinet, integrating the inverter, protection devices and the welding controller. The controller features an intuitive graphical display and provides advanced process control, allowing operators to manage welding parameters quickly and accurately.
The controller includes constant current control, programmable weld schedules, pre-weld and post-weld functions, current ramp-up and ramp-down, pulse welding and electrode wear compensation. Operators can also monitor RMS welding current, machine utilisation and, where required, manage diagnostics and programme settings via optional USB communication.
For applications requiring even greater process control, an optional proportional valve enables the working pressure to be automatically linked to individual welding programmes. Maintaining consistent electrode pressure contributes to improved process stability, repeatable weld quality and better overall production reliability.
Selecting the right MF suspended spot welding gun depends on far more than output power alone. Production volumes, material characteristics, component geometry and integration with automated manufacturing lines or robotic welding cells should all be considered before specifying the equipment. This is why ATS works alongside customers to evaluate every aspect of the application before recommending the most suitable configuration.
| Feature | MF Inverter 3230 | MF Inverter 3233 |
|---|---|---|
| Technology | Medium frequency MF inverter technology | Medium frequency MF inverter technology |
| Rated power | 50 kVA at 50% duty cycle (80 kVA at 20%) | 50 kVA at 50% duty cycle (80 kVA at 20%) |
| Main application | Applications requiring higher electrode force | Applications requiring greater operating flexibility |
| Throat gap / stroke | 155 mm | Double stroke 0–40 mm |
| Maximum electrode force (6 bar) | 380 daN | 300 daN |
| Short-circuit current | 19 kA | 19 kA |
| Arm fitting diameter | 28 mm | 34 mm |
| Recommended configuration | Components requiring higher clamping force and welding pressure | Components requiring improved flexibility and easier access |
If you are looking for a 50 kVA MF inverter suspended spot welding gun for industrial resistance welding, the technical team at ATS Lamberti can help you compare the 3230 and 3233 models, identify the most suitable configuration and provide technical support before and after installation.
Request information about this product
Leave us your details: we will get back to you as soon as possible with all the information about this product.
Products in the same category
Suspended spot welders